Recently, Harvard University's article-by-article interpretation of the FRESH Act has aroused widespread attention in the global food industry. The core controversy of the bill lies in the regulatory loopholes of food chemicals (such as synthetic pigments, PFAS, etc.), especially the GRAS (generally considered safe) exemption mechanism. Although this debate originated in the United States, its impact has spread to the global food supply chain, especially the procurement and upgrading of food processing machinery. For Chinese food machinery companies planning to export or benchmark international standards, understanding this trend and planning ahead is the key to winning the high-end market.
Stricter regulation of food chemistry: the chain reaction of mechanical design
The FRESH Act, if passed, would require food manufacturers to conduct stricter toxicity reviews of all added substances and could ban or restrict the use of some chemicals in food contact materials. This means that mechanical parts that come into direct contact with food - such as conveyor belts, seals, coatings, pipes, etc. - must be replaced with safer alternative materials. For example, traditional rubber seals may contain anti-stick coatings of the PFAS class, while new food-grade silicone or ethylene-propylene-diene (EPDM) rubber is becoming a safer option. Machine manufacturers should pay attention to the latest updates to FDA (US Food and Drug Administration) and European Union EU 10/2011 regulations to ensure that contact materials meet migration limits. In addition, equipment lubricants are also required to use food-grade NSF H1 certified products to avoid potential chemical contamination risks.
Application scenarios: full compliance from raw material handling to packaging
Chemical risks can be introduced at every stage of raw material cleaning, cutting, heat treatment, filling and packaging. For example, in a fried food production line, if a conveyor belt containing PFAS is used, harmful substances may be released at high temperatures. Modular conveyor belts using stainless steel or food-grade plastics (e.g. POM, PVDF) are more stable. In the beverage filling process, the pipeline sealing material needs to be resistant to acid and alkali cleaning agents, while not releasing bisphenol A (BPA) or other endocrine disruptors. For baking machinery, the non-stick coating of molds is shifting from fluoropolymers to ceramic-based coatings. When purchasing equipment, purchasers should require suppliers to provide detailed material compliance statements and pay attention to whether the equipment is easy to disassemble and wash to reduce secondary pollution caused by cleaning agent residues. In addition, when integrating a CIP system, materials that are resistant to chemicals should be selected and the cleaning process should be optimized to reduce water and chemical consumption.
Selection Suggestions: Building a "Mechanical Line of Defense" for Food Safety
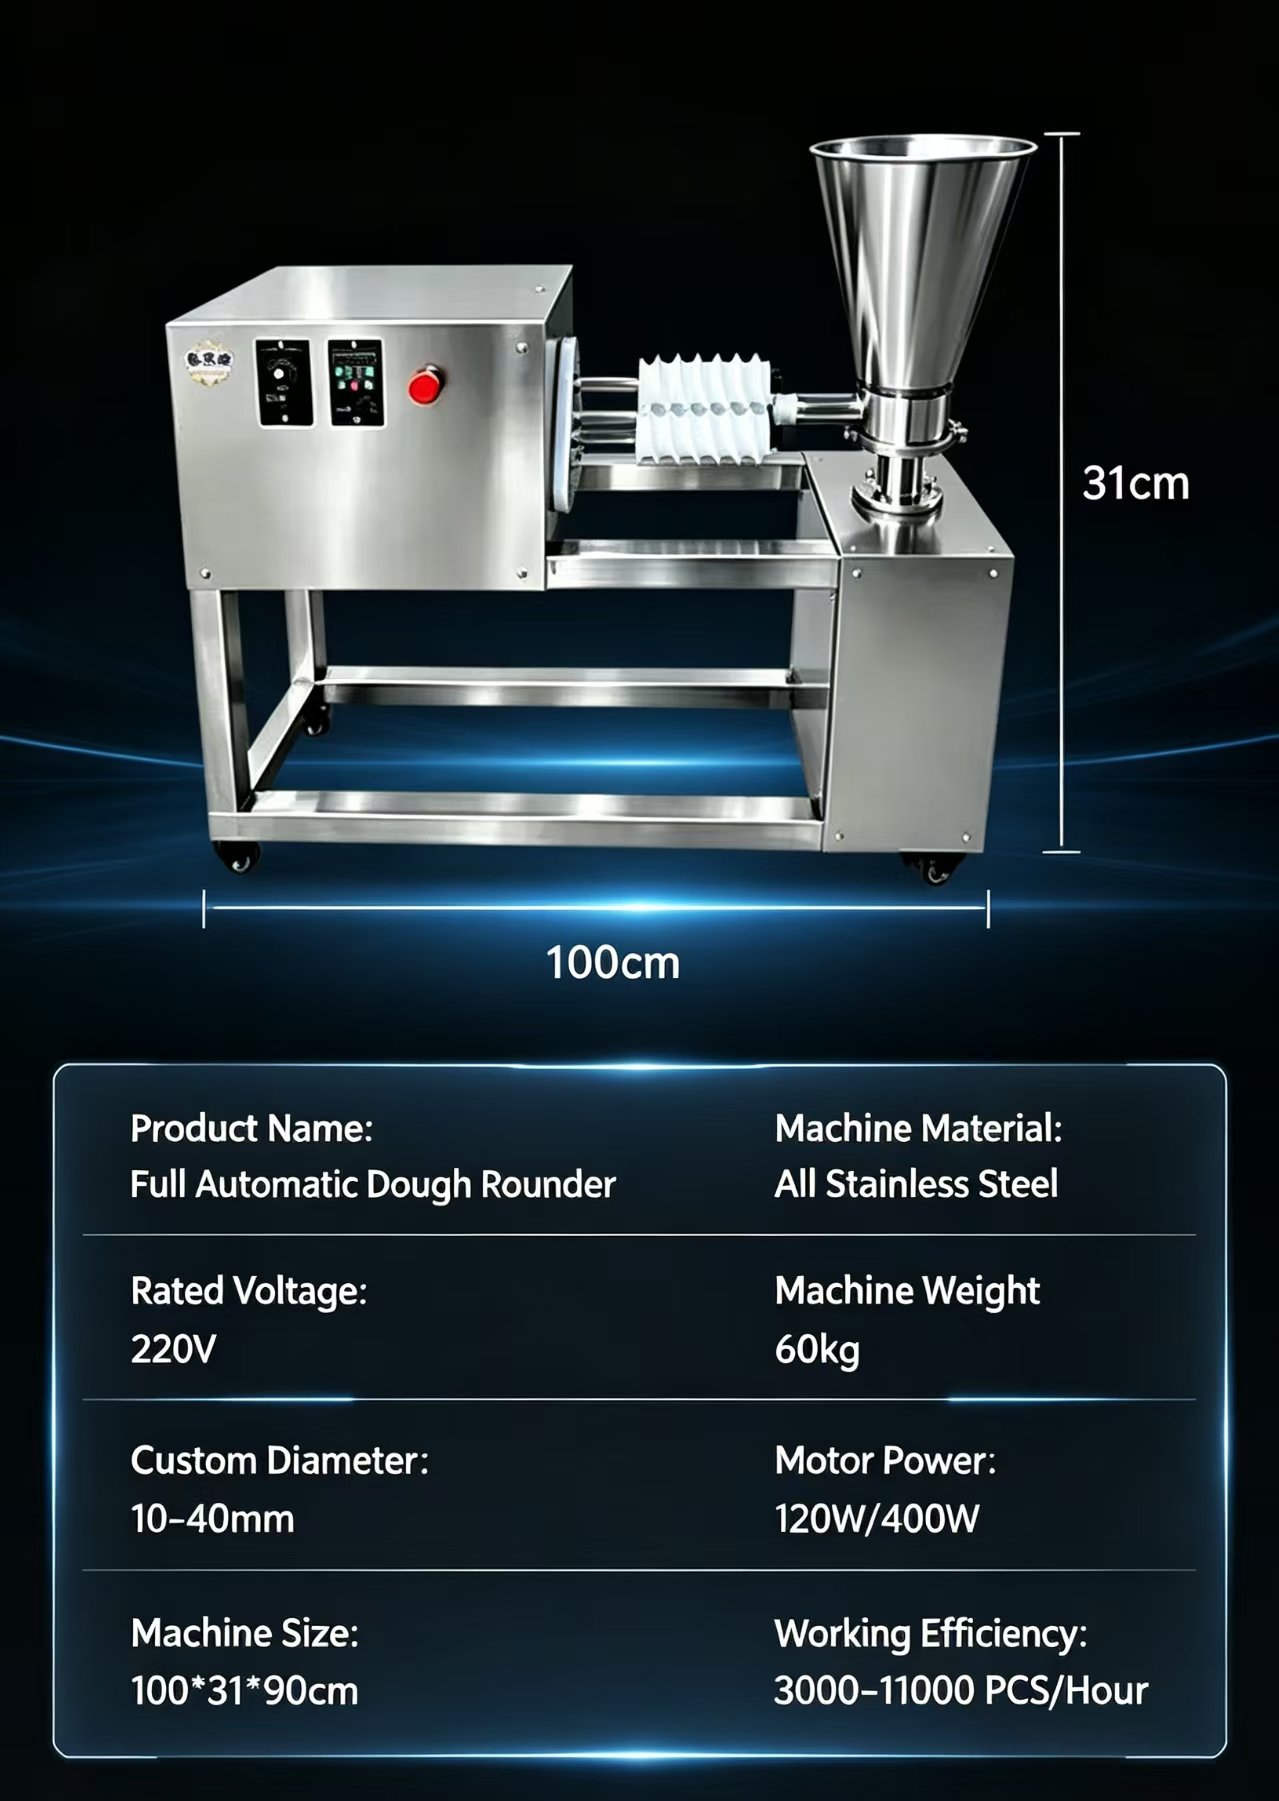
Faced with global regulatory differences, food machinery buyers should establish a multi-dimensional evaluation system. First, confirm whether the equipment has passed the certification of the main target market, such as the American Baking Society (BISSC), the European Union CE and the US 3-A hygiene standard. Second, review the "traceability" of the machinery, that is, whether the supplier of key components provides proof of material composition. For example,Check out our food-grade conveyor equipmentFirst, all contact components are provided with FDA compliance documents. Second, consider the modular design of the equipment, which makes it easy to replace specific components in the future according to regulatory changes, rather than scrapping the entire machine. Finally, focus on energy efficiency and wastewater treatment design, as chemical bans are often accompanied by stricter environmental protection requirements. We recommend adding a "compliance change clause" to the procurement contract, so that if the target market regulations are updated, the supplier needs to provide a modification plan.
From Compliance to Competitiveness: The Value of Proactive UpgradingAlthough stricter regulations increase short-term costs, companies that proactively comply will gain significant competitive advantages. For example, equipment free from PFAS and BPA can serve as a "door opener" for exporting to European and American markets and help enhance brand image. At the same time, reducing the use of chemicals also reduces occupational health risks for workers and waste disposal costs. In our recently published industry technical article, we analyzed in detail the impact of the new EU regulations on food contact materials on production line design. We recommend that companies regularly attend international food processing exhibitions and pay attention to the latest breakthroughs in materials science, such as bio-based plastics and nano-ceramic coatings. By integrating food safety concepts into mechanical design and procurement decisions, companies can not only avoid trade risks but also build long-term, sustainable competitiveness.
In short, the debate over the FRESH Act is just a microcosm of the global upgrading of food safety supervision. For purchasers and manufacturers of food machinery, this is both a challenge and an opportunity to optimize production lines and enhance product added value. By selecting compliant materials, optimizing hygienic design, and establishing traceability systems, companies can confidently adapt to the changing global regulatory environment and ensure the safety and quality of their final products. Take action immediately and turn compliance into your core competitiveness.